
PipeWIZARD iX AUT System
Rugged Phased Array System for Girth Weld Validation
PipeWIZARD-iX Automated Inspection
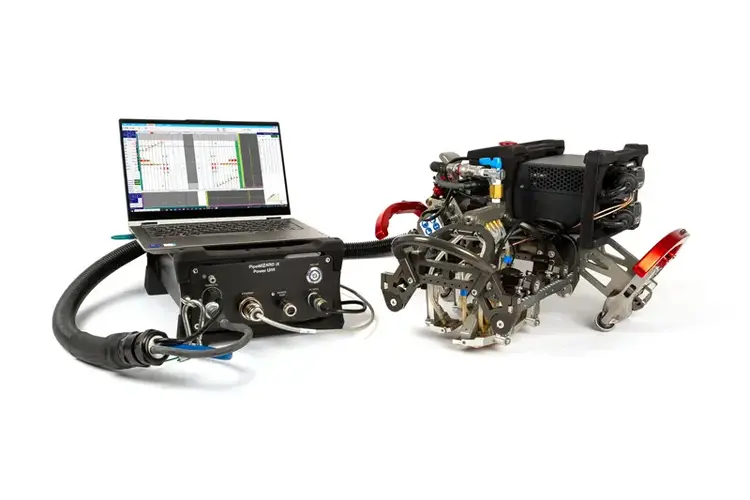
PipeWIZARD™ iX Automated Ultrasonic System for Girth Weld Inspection
The PipeWIZARD™ iX phased array ultrasonic testing system helps pipeline companies ensure the reliable validation of girth welds during the construction process. Equally rugged and compact, the PipeWIZARD iX system is designed to facilitate both onshore and offshore pipeline inspections. A highly efficient automated ultrasonic testing (AUT) solution, this powerful multitechnology detection system reveals defects in girth welds and the heat-affected zone (HAZ) so they can be quickly analyzed and evaluated.
High-Performance Instrument for Standard and Advanced Inspections
The PipeWIZARD iX system is built to resist vibrations, shocks, and electromagnetic interference, and it can withstand extreme temperatures. Thanks to its compact yet robust design, the PipeWIZARD iX system is also easy to transport and manipulate with confidence.
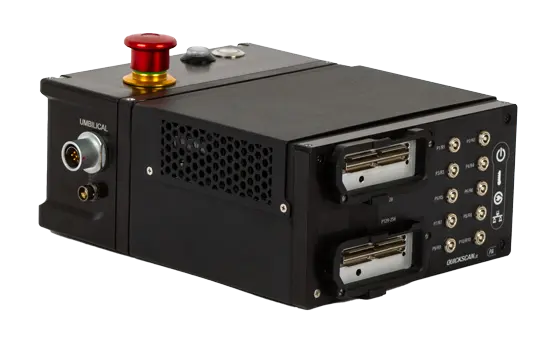
Lighter than its predecessor, the PipeWIZARD iX system’s data acquisition unit is integrated onto the scanner, making it easier to set up and operate. Featuring more powerful electronics and more input channels, the QuickScan iX PA 64:256 data acquisition instrument boosts the PipeWIZARD system’s capabilities and efficiency, improving the coverage capacity and supporting advanced ultrasonic inspection techniques.
Improved Ease of Use and On-Site Efficiency
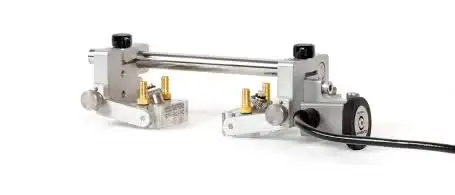
The optimized hardware design of the PipeWIZARD iX system provides increased setup flexibility and adaptability. Additional umbilical cable lengths, quick-latching connectors, and configurable probe modules increase your ability to accommodate the PipeWIZARD iX setup to varying inspection needs and environments. Its narrower band also significantly reduces coating cutback requirements versus its predecessor.
The PipeWIZARD iX system enables onsite inspection personnel to work together more easily and efficiently. Integrated indicator lights and software functions ease the communication between the scanner technician and operator, so the inspection goes smoothly, even under challenging conditions.
Optimized Inspection and Analysis Workflow
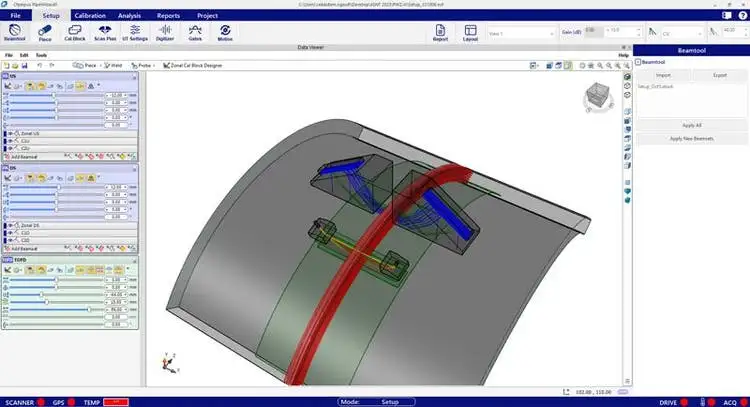
Thoughtfully designed to reflect the key requirements for reliable and code-compliant girth weld validation, the PipeWIZARD iX companion software is easier to use yet features more advanced and sophisticated tools, including:
- Embedded ES BeamTool software
- Calibration block designer
- Encoder auto-calibration
- Analysis assistance
For increased data accessibility and versatility, the QuickScan iX PA acquisition unit saves data files in an open file format, facilitating custom software development. If customization is an aspect that interests you, talk to your Evident representative for more details.
Applications
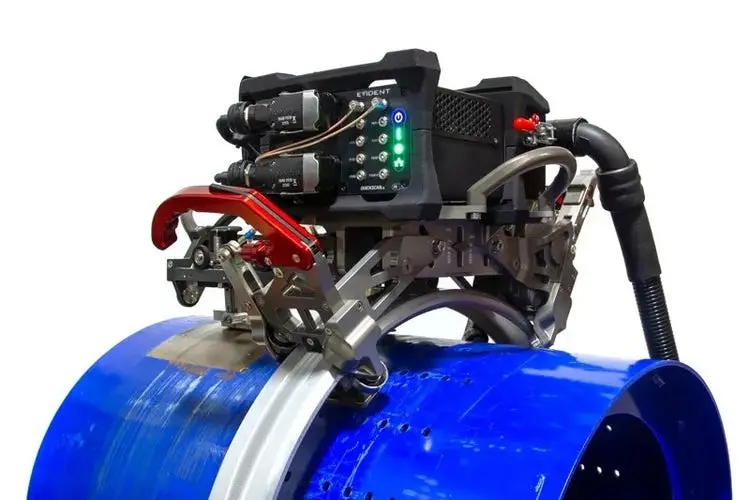
Complete Girth Weld Inspection System
The PipeWIZARD iX girth weld inspection system is built for demanding and extreme conditions, from cold subarctic regions to hot deserts. Detecting defects including lack of fusion, incomplete penetration, porosity, burn through, undercut, hi-low, crack, cold lap, inclusion, etc. the PipeWIZARD iX system adapts to all circumferential weld configurations:
Any weld profile type, including J-bevel, V-bevel, double V, X, etc.
Pipe wall thicknesses typically from 6 mm (0.25 in.) to more than 35 mm (1.4 in.); options are available for thicker pipes.
Pipe diameters from 168 mm (6.625 in.) to 1524 mm (60 in.).
Pipe materials from standard carbon-steel to more complex configurations, including Inconel, and cladded pipe.
Automated Ultrasonic Testing (AUT)
For pipeline girth weld inspection, automated ultrasonic testing (AUT) is the replacement of choice for traditional radiography.
Some clear advantages of AUT over radiography:
- No radiation risks for personnel, no chemicals, or environmental concerns
- Comparatively short inspection cycle time enabling high productivity
- Better detection and sizing accuracy, leading to lower rejection rates
- Satisfies Engineering Critical Assessment (ECA) acceptance criteria with measurement of vertical height and depth of indications
- Real-time analysis from smart output display
- Data and inspection reports
- No licensing required
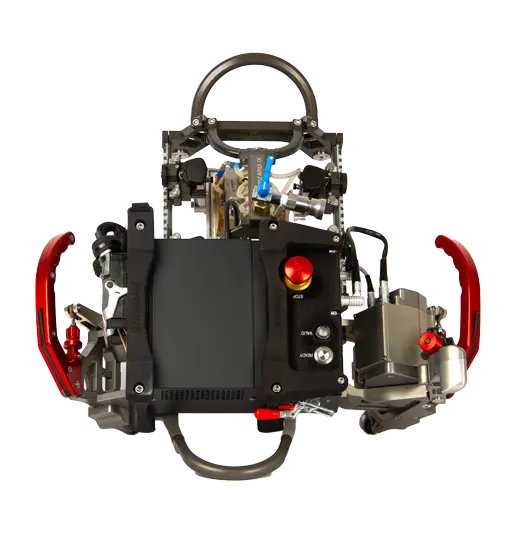
Multitechnology Inspection Capabilities
Leverage the versatile advanced phased array and conventional ultrasonic technology of the PipeWIZARD iX system:
- Zone discrimination―each zone, approximately equal to a welding pass, is inspected individually with a PA pulse-echo or pitch-catch technique, enabling full coverage of the bevel area and the volume of the weld with accurate flaw sizing.
- Time-of-flight diffraction (TOFD)―used to confirm indications seen on the strip chart or to improve detection and sizing on small or misoriented indications.
- Phased array (PA)― conventional PA techniques, such as sectorial, linear, or compound scans, can be used as complementary methods or to inspect weld configurations where zone discrimination is not optimal.
- Conventional UT―for detecting transverse flaws in a pitch-catch configuration, measuring wall thickness, inspecting the upper area of the weld with creeping waves, etc.
- Total focusing method (TFM) compatible―the powerful QuickScan iX PA data acquisition instrument is capable of supporting the complex firing patterns required for advanced techniques such as TFM.
Code Compliance for Girth Weld AUT Inspections
Confidently validate girth welds according to international standards and regulations governing both the offshore and onshore pipeline industry. The PipeWIZARD iX system enables you to perform AUT inspections that comply with the following codes:
- ASTM E-1961 code (covering key elements of AUT of girth welds, including zone discrimination, rapid data interpretation, specialized calibration blocks, and configuration procedures)
- API 1104 standard (by inference)
- DNV-OS-F101 standard (the offshore AUT code)
When your company’s specifications demand it, you can increase the accuracy of your flaw sizing and achieve a level of resolution that exceeds these code requirements.
Key Features of the PipeWIZARD iX System
- Integrated QuickScan iX PA data acquisition instrument accommodating PA probes with up to 256 elements and up to 10 independent UT probes.
- Acquisition unit conveniently mounted on the scanner, eliminating signal attenuation due to a long umbilical cable.
- Embedded with Eclipse Scientific’s BeamTool software for inspection and analysis, offering the zonal discrimination technique including a zonal cal block designer.
- Software equipped more automated tools:
- Auto-setup
- Auto-layout
- Encoder auto-calibration
- Assisted analysis
- Auto-sizing in height and length
- Quick-connect umbilical cable is light, swivels easily, and come in various lengths, simplifying cable management and improving the signal-to-noise ratio (SNR).
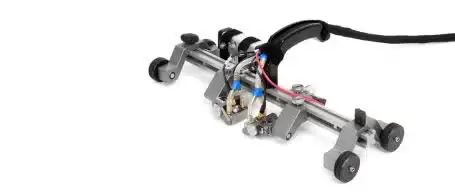
Length options: 10 m, 20 m, 30 m, and 50 m (32.8 ft, 65.6 ft, 98.4 ft, and 164 ft). - Scanner carriage is easy to set up and operate with its improved clamping and drive wheel adjustment mechanisms, making it easier to adapt to different pipe diameters.
- Minimal parts requiring low maintenance and designed for durability in all conditions.
- Width of the band is reduced, lowering the required coating cutback (shorter coating cutback than the previous model); the same band can be used for 2 pipe diameters using the optional spacers .
- Probe module holds up to 12 probes; you can easily remove and add sections as required.
- The smart spring-loaded arms (low maintenance) holding the probes are equipped with a pointer to set accurately the index offsets.
- Direct communication between scanner technician and operator (“Ready” button and scan validation light).
- GPS option to record geographic position in the data file.
- System hardware is ready to support FMC/TFM (upcoming software feature).
Technical Specifications
| Size | Full scanner with handles / 577 mm × 578 mm × 210 mm (22.7 in. × 22.7 in. × 8.3 in.) |
|---|---|
| Acquisition unit | 243 mm × 188 mm × 100 mm (9.6 in. × 7.4 in. × 3.9 in.) |
| Weight | Full scanner with handles / 18 kg (40 lb) |
| Acquisition unit | 4.8 kg (10.6 lb) |
| Pipe Diameter Range | From 168 mm (6.625 in.) to 1524 mm (60 in.) |
| Maximum Scanning Speed | 100 mm/s (3.9 in./s) |
| Environment | Storage temperature / −30°C to 60°C (−22°F to 140°F) |
| Operating Temperature | −30°C to 50°C (−22°F to 122°F) |
| Max relative humidity | 90% noncondensing |
| Pollution degree (level) | 4 |
| Altitude | Up to 2000 m (6561 ft) |
| IP rating | IP65 |
| Installation category | III |
| Ethernet Connectivity | Ethernet interface / 1000BASE-T (bandwidth of 1000 Mbps) |
| Cable length | 30 m max. (100 ft) |
| Cable type | Category 5e or higher, shielded |
| Transfer rate on Ethernet cable | 940 Mbps max. |
| Connector | Female RJ-45, shielded |
| DC Power Requirements | Voltage / 24 VDC ±5% |
| Max. power consumption | 360 W |
| System | Warm-up time / None |
| Probe Connectors | 2 phased array (IPEX) and 10 conventional UT (LEMO) |
| Positioning System | External GPS (optional) |
| Temperature Sensor | Thermocouple for wedge temperature monitoring |
| Techniques | Zone discrimination, PA, TOFD, UT |
| Parameter | PA / UT |
|---|---|
| Number of Focal Laws | 1024 / N/A |
| Pulse Output (into a 50 Ω) ±10% | 5, 10 , 20, 40, 60, 80, 90 volts peak-to-peak (Vpp) for a bipolar pulse |
| Pulse Output (in High Impedance) | 8.5, 17, 33, 67, 100, 134 and 150 volts peak-to-peak (Vpp) |
| Number of Pulsers | 64:256PR with parallel firing / 10 |
| Number of Elements | 256 / N/A |
| UT Channels | N/A / P/E: up to 10 and P/C: up to 5 |
| Pulse Width/Step (Precision of 5 ns or ±10%) | 30 ns to 1000 ns (steps of 5 ns) |
| Fall Time | 15 ns for a 40 Vpp bipolar pulse |
| Pulse Shape | Bipolar, positive, and negative square pulse |
| Output Impedance | 25 Ω / 39 Ω |
| Parameter | PA / UT |
|---|---|
| Gain Range/Increment | 0 dB to 80 dB (44 dB analog + 36 dB digital) |
| Gain Resolution | 0.1 dB |
| Maximum Input Signal | P/E & P/C: 1.05 Vpp / P/E & P/C: 1 Vpp |
| Input Impedance | P/E & P/C: 63Ω ±15% / P/E & P/C: 132 Ω ±1.5 Ω |
| Gain Precision between Channels (at 20 dB) | 0.5 dB / 0.1 dB |
| Crosstalk Isolation between Channels | >45 dB at 5 MHz / >80 dB at 5 MHzOnly for channel pairs specified in the user manual. |
| System Bandwidth (−3 dB) ±10% | 0.68 MHz to 22.3 MHz |
| Elementary A/D Converter | PA: 14 bits, 120 MSPS; UT: 14 bits, 120 MSPS |
|---|---|
| Digitizing Frequency | 100 MHz |
| Amplitude Resolution | 8 bits / 16 bits |
| A-Scan Height | Up to 800% |
| Global Data Throughput | Up to 90 MB/s |
| Maximum Pulse Repetition Frequency (PRF) | 25 kHz |
| Maximum Number of A-Scan Samples | 16380 |
| Acquisition Depth | 163.8 µs without compression |
| Compression | 1 to 2000 |
| Averaging | 1, 2, 4, 8, 16, 32, 64 |
| Rectifier | RF/FW/HW+/HW− |
| Digital Filtering | Low-pass: 2, 4, 7.45 MHzBand-pass: 2 (1–3.5), 4 (2–6.5), 5 (2.5–8), 8 (4–12), 10 (5–16), 12 (6–18) MHzHigh-pass: 4, 6, 8, 10 MHz |
| EMC | EN IEC 61326-1:2021, EN 61000-3-2:2014, EN 61000-3-3:2013USA: FCC 47 CFR Part 15, Subpart B – VerificationCanada : ICES-001 Issue 5 July 2020 |
|---|---|
| GPS | ETSI EN 301 489-19 V2.2.1 (2022-09) |
| Phased Array | ISO-18563-1 (2022) |
| UT | ISO-22232-1 (2020) |
Applications
Inspection scenarios where the PipeWIZARD iX AUT System is used: